Multi-Brand Authorized Coverage — Procure the 120RUB40 alongside other metallurgical spares in a single consolidated shipment without juggling multiple vendors.
Technical Specifications
| Parameter |
Value |
| Designation |
120RUB40 |
| Bearing Type |
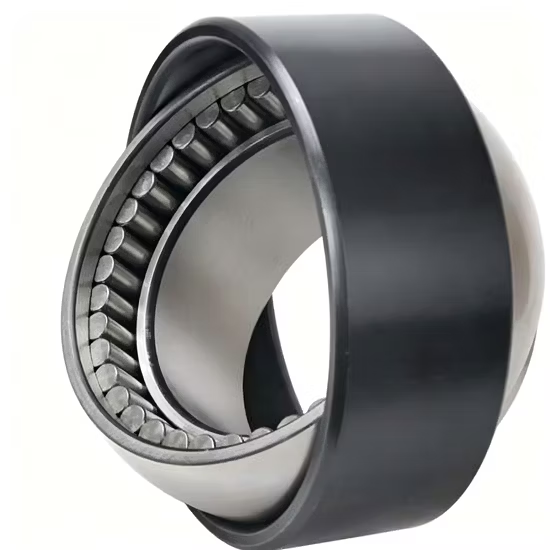
Spherical-Seat Cylindrical Roller Bearing |
| Bore Diameter (d) |
120 mm |
| Application |
Continuous Caster Free Side |
| Material |
Available in standard bearing steel or specialized high-temperature variants |
| Clearance Class |
C3 / C4 (selected based on thermal expansion requirements) |
| Precision Class |
P0 / P6 (matched to continuous caster alignment tolerances) |
Note: The RUB and 40 suffixes are unverified and require manufacturer catalog confirmation prior to final order placement.
Application Suitability
| Industry |
Typical Applications |
| Steel and Metallurgy |
Continuous caster free side roll guidance and support |
| Industrial Equipment |
Heavy-duty material handling mechanisms under high thermal load |
Why a Matched Base Number Still Leads to 120RUB40 spherical-seat cylindrical roller bearing Failure
Internal geometry and clearance mismatches cause thermal binding long before the steel itself yields.
In continuous casting environments, replacing a worn unit with one that only matches the base designation is a frequent trap. I have seen production lines halt because a standard clearance was installed where a C3 or C4 was mandatory for thermal expansion. When the inner ring expands under extreme heat without adequate internal clearance, the rollers bind against the raceway. This leads to catastrophic cage failure and unplanned downtime, a scenario detailed in rolling bearing failure mode classification per ISO 15243 [NEED_CITE: rolling bearing failure mode classification per ISO 15243]. Sourcing the exact 120RUB40 spherical-seat cylindrical roller bearing requires verifying the internal design, not just the stamped numbers.

Aligning the 120RUB40 spherical-seat cylindrical roller bearing with Caster Free Side Demands
The continuous caster free side operates under intense thermal gradients and heavy radial loads. A 120RUB40 spherical-seat cylindrical roller bearing accommodates the inevitable misalignment of the roll segments while supporting the massive weight of the solidifying steel. Our technical review ensures the spherical seat geometry and internal clearance perfectly match your specific operating temperature and load profile.
Thermal Gradients and Lubrication Survival in Metallurgical Zones
The free side of a continuous caster exposes components to severe heat, demanding careful consideration of thermal expansion and lubrication breakdown. Standard greases will carbonize, requiring specialized high-temperature lubricants or oil-air systems to maintain a protective film. The spherical outer ring helps distribute contact stresses evenly, but if the internal clearance is not upgraded to compensate for the heat, the lubricant is quickly squeezed out. Proper seal selection is equally critical to keep abrasive scale and cooling water out of the raceway without generating excessive friction heat [NEED_CITE: bearing seal friction and contamination ingress in steel mills].
Decoding the Spherical Seat and Internal Geometry
The 120 mm bore diameter provides a substantial cross-section for heavy radial loads typical in metallurgical equipment. The spherical-seat outer ring design is crucial here; it allows the bearing to self-align within the housing, compensating for the shaft deflection and housing misalignment common in continuous caster frames. Selecting the correct clearance class—typically C3 or C4 for these high-temperature zones—ensures the internal geometry maintains optimal rolling contact even when the inner ring expands significantly more than the outer ring. The cylindrical roller profile is optimized to handle the pure radial forces while the spherical exterior manages the angular discrepancies.
The Hidden Costs of Overlooking Suffix and Clearance Details
Installing a bearing with incorrect internal clearance or a mismatched spherical seat geometry leads to rapid thermal binding and premature spalling. This is not just a component replacement issue; it triggers cascading damage to the roll segments and housing, resulting in extensive unplanned downtime. According to ISO 281 standards for dynamic load ratings and rating life, operating a bearing under bound conditions drastically reduces its calculated fatigue life [NEED_CITE: ISO 281 dynamic load rating and rating life calculation methods]. The financial impact of a halted casting line far exceeds the cost of precise technical verification upfront.
Securing Precision Through Authorized Technical Verification
We prevent cross-reference errors by matching the internal design, clearance, and spherical seat geometry, rather than relying solely on the base designation. For the 120RUB40, this means confirming the exact suffix requirements to avoid the thermal binding that plagues standard clearance replacements. Our authorized channel procurement guarantees genuine products with traceable metallurgy, eliminating the risk of counterfeits with soft inner rings that fail under heavy caster loads. Every shipment includes comprehensive documentation, ensuring your maintenance team receives exact dimensional and running accuracy inspection reports before the bearing reaches the shop floor.
Documentation & Authenticity
- Certificate of Conformity confirming the exact 120RUB40 designation and material grade.
- Original manufacturer batch and lot traceability for full metallurgical accountability.
- Official app QR verification to instantly validate the authenticity of the spherical-seat bearing.
- Material test report verifying the heat treatment and hardness of the inner and outer rings.
- Dimensional and running accuracy inspection report confirming P0 or P6 tolerances prior to dispatch.
- Country-of-origin documentation ensuring compliance with your facility’s procurement mandates.
Storage, Handling & Mounting
- Store the 120RUB40 in its original packaging to protect the spherical outer ring surface from humidity and physical damage.
- Maintain a stable storage temperature to prevent condensation inside the bearing, which compromises the anti-corrosion coating before installation.
- Use clean gloves when handling the 120 mm bore to prevent sweat-induced corrosion on the precision-ground inner ring raceway.
- Utilize induction heating for the inner ring mounting, strictly monitoring the temperature to preserve the selected C3 or C4 clearance class.
- Apply the specified high-temperature lubricant immediately after mounting if the bearing is supplied open, ensuring complete roller coverage.
- Verify the spherical seat alignment in the housing before final locking, preventing edge loading on the cylindrical rollers.
Initiating Your Technical Inquiry
To ensure the 120RUB40 spherical-seat cylindrical roller bearing perfectly matches your continuous caster, please provide the specific radial loads, operating temperatures, and rotational speeds. Sharing the OEM equipment number or existing housing dimensions allows our engineering team to perform a precise cross-reference and L10 life calculation. Detailing the environmental exposure, such as cooling water spray or abrasive scale, helps us confirm the optimal seal and material configuration for your application.
Frequently Asked Questions
Q: How can I verify the batch traceability of the 120RUB40 bearings I receive?
A: Every 120RUB40 spherical-seat cylindrical roller bearing we supply includes original manufacturer batch and lot traceability. You can verify the authenticity directly through the brand’s official mobile application by scanning the QR code on the packaging. This ensures the internal geometry and material specifications match the factory records, protecting your continuous caster from counterfeit risks.
Q: Why do cross-reference errors cause thermal binding in continuous caster free side applications?
A: Cross-reference errors often match the base 120 mm bore but overlook the necessary C3 or C4 clearance required for thermal expansion. When a standard clearance bearing is used in the high-heat environment of a continuous caster, the inner ring expands and eliminates the internal gap. This causes the cylindrical rollers to bind against the raceway, leading to rapid overheating and catastrophic cage failure.
Q: What internal design differences must I check when replacing continuous caster bearings?
A: Beyond the base designation, you must verify the spherical seat geometry, internal clearance class, and cage material. The spherical exterior must match the housing curvature to allow proper self-alignment, while the clearance must accommodate the specific thermal gradient of your caster zone. We review these exact parameters to ensure the replacement 120RUB40 performs reliably under your specific load and temperature conditions.
Q: How do I select the correct clearance for high-temperature metallurgical applications?
A: Selecting the correct clearance involves calculating the temperature differential between the inner ring, outer ring, and housing. In continuous caster applications, the inner ring typically runs hotter, requiring a C3 or C4 clearance to prevent thermal binding. Provide your operating temperature data and cooling conditions, and our technical team will recommend the precise clearance class to maintain optimal rolling contact.
Q: What documentation is provided to ensure quality assurance for steel mill spares?
A: We provide a comprehensive documentation package including a Certificate of Conformity, material test reports, and dimensional inspection reports confirming the running accuracy of the 120RUB40. You also receive original batch traceability and country-of-origin documents. This complete paper trail ensures full compliance with your maintenance standards and guarantees the bearing’s suitability for critical metallurgical equipment.