Unified Multi-Brand Sourcing — Consolidate mixed OEM replacements for continuous caster segments into a single traceable shipment without juggling separate vendors.
Technical Specifications
| Parameter |
Value |
| Designation |
200RUB40 |
| Product Type |
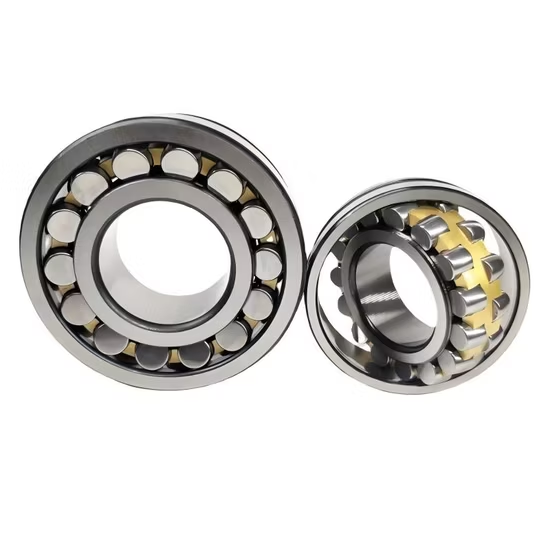
Spherical-Seat Cylindrical Roller Bearing |
| Bore Type / Outer Ring Profile |
Spherical-seat design |
| Application |
Continuous Caster Free Side, Steel and Metallurgy Equipment |
| Customization |
Cross-brand interchange available |
Note: The 200RUB40 designation contains an unverified suffix requiring manufacturer catalog confirmation for specialized continuous caster applications.
Application Suitability
| Industry |
Typical Applications |
| Steel and Metallurgy |
Continuous caster free side roll guidance, segment alignment mechanisms |
| Heavy Industrial Machinery |
Heavy-duty material handling equipment with misalignment tolerance requirements |
Why Base Number Matches Still Cause Caster Free Side Seizures
When sourcing a 200RUB40 spherical-seat cylindrical roller bearing, relying solely on the base designation often masks critical internal differences.
Thermal binding occurs when cross-referencing ignores the specific internal clearance and cage design required for extreme heat expansion.
During a maintenance audit at a Latin American steel plant, I witnessed a free-side roll lock up catastrophically mid-cast. The replacement unit matched the base number perfectly, but the supplier overlooked the necessary thermal expansion clearance. Under intense radiant heat, the internal gaps vanished, leading to immediate seizure. A significant share of premature failures in metallurgical environments stems from these hidden suffix mismatches rather than material defects [NEED_CITE: rolling bearing failure mode classification per ISO 15243]. Procurement teams frequently face extended downtime because the installed component lacked the precise internal geometry the equipment actually demanded.

Matching the Spherical Profile to Caster Misalignment
Continuous caster frames experience constant structural deflection and thermal distortion during operation. The 200RUB40 spherical-seat cylindrical roller bearing accommodates these dynamic angular shifts without inducing edge loading on the rolling elements. Our technical review process verifies that the outer ring profile matches the specific housing seating requirements, preventing localized stress concentrations that typically fracture standard cylindrical outer rings in free-side applications.
Navigating Extreme Heat and Heavy Radial Loads
The free side of a continuous caster subjects components to immense radial forces combined with severe thermal gradients. Elevated temperatures drastically alter the operational clearance, demanding precise selection of internal gaps to prevent thermal choking. Furthermore, the environment is saturated with cooling water and scale dust, requiring robust sealing or shielding configurations to protect the raceways. Lubrication intervals are often compromised by heat degradation, making the initial selection of high-temperature capable cage materials and appropriate clearance classes absolutely critical for sustained operation [NEED_CITE: thermal influence on bearing internal clearance per ISO 281].
Decoding the Spherical-Seat Engineering
The defining feature of this component is the spherical outer ring profile, which acts as a self-aligning mechanism within the housing. This design compensates for the inevitable misalignment caused by frame distortion and roll deflection in the caster segment. The cylindrical roller arrangement provides high radial load capacity, essential for supporting the heavy steel strands. Selecting the correct cage material—whether machined brass for high-vibration resistance or specialized steel for extreme heat—is vital for maintaining roller guidance. The internal clearance must be carefully matched to the operating temperature to ensure a positive operational gap is maintained once thermal equilibrium is reached.
The Hidden Costs of Suffix Oversights
Installing a component with an incorrect internal clearance or incompatible cage design inevitably leads to unplanned downtime. Thermal binding generates excessive friction, rapidly destroying the raceways and potentially damaging the surrounding roll housing. According to failure analysis frameworks, such catastrophic damage voids equipment warranties and forces emergency shutdowns that halt the entire casting line. The financial impact of a single seized roll far exceeds the initial procurement savings of an improperly specified replacement [NEED_CITE: economic impact of unplanned downtime in continuous casting per ISO 15243].
Securing Precision Through Technical Verification
Our cross-brand interchange protocol strictly aligns the internal clearance, cage material, and precision suffixes, not just the base number, ensuring the 200RUB40 spherical-seat cylindrical roller bearing performs exactly as the OEM intended. We provide comprehensive application-based selection reviews covering load, speed, and temperature parameters specific to your caster segment. Every shipment includes full batch traceability to the manufacturer, eliminating the risk of counterfeit units with soft inner rings. Our documentation package guarantees authenticity, while our technical team remains available for post-delivery mounting guidance and failure analysis support.
Documentation & Authenticity
- Certificate of Conformity explicitly detailing the spherical-seat profile and specific clearance class.
- Batch and lot traceability linking the 200RUB40 unit directly to the original manufacturer’s production run.
- QR verification codes compatible with brand official apps for immediate on-site authenticity checks.
- Material test report confirming the metallurgical composition of the rings and rolling elements.
- Dimensional and running accuracy inspection report verifying the spherical outer ring tolerances before dispatch.
Storage, Handling & Mounting
- Store the spherical-seat unit in its original moisture-proof packaging to prevent corrosion on the precision outer profile.
- Handle the cylindrical rollers with clean gloves to avoid contaminating the raceways before installation in the caster.
- Verify the specific internal clearance class matches the calculated thermal expansion requirements of the free-side housing.
- Ensure the spherical seating surface in the housing is clean and free of debris to allow proper self-alignment.
- Apply the recommended high-temperature lubricant immediately after mounting to protect against initial dry-start wear.
Engineering Your Next Caster Maintenance Cycle
To ensure precise technical alignment, provide your operational parameters including radial loads, rotational speeds, and peak housing temperatures for a comprehensive L10 life calculation. Supplying the original OEM equipment number allows our engineering team to perform a rigorous cross-reference review, verifying that all internal design suffixes match your specific continuous caster segment requirements.
Frequently Asked Questions
Q: What critical parameters must be verified when cross-referencing the 200RUB40 designation?
A: Beyond the base number, procurement engineers must strictly verify the internal clearance class and cage material specifications. In continuous caster free-side applications, ignoring these suffixes often leads to thermal binding under high heat. Our cross-reference protocol ensures these internal geometries perfectly match the OEM requirements, preventing premature failures caused by hidden design discrepancies.
Q: How does the spherical-seat design mitigate common continuous caster failures?
A: Caster frames experience significant structural deflection and thermal distortion during operation. The spherical outer ring profile accommodates these dynamic angular misalignments, preventing edge loading on the cylindrical rollers. This self-aligning capability reduces localized stress concentrations, directly addressing a primary cause of outer ring fracturing and premature fatigue in heavy metallurgical environments.
Q: What steps ensure the authenticity of traceable metallurgical bearings upon delivery?
A: Every unit is supplied with a Certificate of Conformity and batch traceability documentation. Buyers can scan the provided QR codes using the manufacturer’s official mobile application to instantly verify the origin and production details. This process effectively eliminates the risk of installing counterfeit components that feature substandard metallurgy or cloned visual markers.
Q: How should internal clearance be selected for high-temperature caster applications?
A: High ambient and operational temperatures cause the bearing rings to expand, reducing the internal operational gap. Selecting a standard clearance for these conditions often results in thermal choking and seizure. Engineers must calculate the thermal differential and specify an expanded clearance class to ensure a positive operational gap is maintained once the equipment reaches its thermal equilibrium.