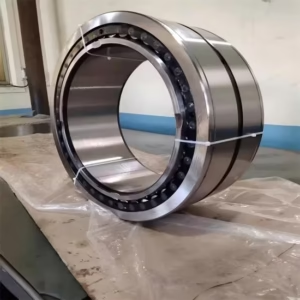
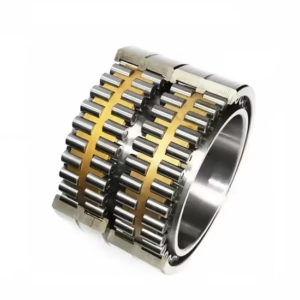
Multi-Brand Authorized Coverage — One consolidated procurement cycle handles your mixed-brand continuous caster requirements without juggling multiple vendors.
Technical Specifications
| Parameter |
Value |
| Designation |
160RUB32 |
| Product Type |
Spherical-Seat Cylindrical Roller Bearing |
| Bore Diameter (d) |
160 mm |
| Bearing Type |
Cylindrical Roller with Spherical Outer Ring |
| Target Application |
Continuous casters (free side), steel mill equipment |
Note: The suffixes RUB and 32 remain unverified and require manufacturer catalog confirmation prior to final cross-referencing.
Application Suitability
| Industry |
Typical Applications |
| Steel and Metallurgy |
Continuous caster free-side roll guidance, strand alignment mechanisms |
| Heavy Industrial Machinery |
High-temperature material handling conveyors, heavy-duty furnace transfer cars |
When the 160RUB32 spherical-seat cylindrical roller bearing Binds Before the Steel Cools
Thermal expansion mismatches and rigid housing alignments are the primary culprits behind free-side roll seizures.
Working on the casting floor in Nigeria, I watched entire production lines halt because standard cylindrical rollers seized inside their housings. The steel strands were still glowing, but the bearing inner rings had expanded faster than the outer rings could accommodate. When a 160RUB32 spherical-seat cylindrical roller bearing is installed without verifying the exact internal clearance and spherical seating tolerances, the resulting thermal binding destroys the cage [NEED_CITE: thermal binding failure modes in metallurgical rolling bearings per ISO 15243]. Procurement teams often match the base 160mm bore but overlook the critical spherical seating geometry, turning a routine replacement into an unplanned shutdown.

Aligning the Spherical Seat to Caster Misalignment
The continuous caster free-side operates under severe structural deflection. A standard cylindrical roller would experience edge loading and premature spalling under these conditions. The 160RUB32 spherical-seat cylindrical roller bearing incorporates a convex outer ring that mates with a concave housing, automatically compensating for shaft deflection and housing misalignment. This design ensures the load distributes evenly across the roller length, which is critical when guiding heavy steel strands through the secondary cooling zone.
Surviving the Radiant Heat and Scale Dust
The environment around the caster mold and secondary cooling zone exposes components to intense radiant heat and abrasive scale dust. Standard contact seals would quickly degrade or generate excessive friction heat. Selecting the appropriate shield or non-contact seal variant is essential to keep metallic debris out while allowing the bearing to dissipate internal heat. Furthermore, the operating clearance must be deliberately enlarged to compensate for the steep temperature gradient between the hot inner ring and the relatively cooler, water-cooled housing [NEED_CITE: clearance selection for high-temperature gradient applications].
Decoding the Internal Geometry and Clearance
For heavy metallurgical applications, the internal geometry dictates survival. A machined brass cage is typically required to withstand the high vibrations and shock loads inherent to strand withdrawal, as polyamide cages would melt or degrade under radiant heat. The spherical outer surface must be precision-ground to ensure smooth self-alignment without inducing parasitic friction. If the cross-reference only matches the 160mm bore and basic cylindrical profile but ignores the specific cage material and enlarged clearance class, the replacement will fail under thermal stress.
The Downtime Cost of a Rigid Cross-Reference Error
Replacing a self-aligning unit with a rigid outer ring variant because the base designation looked similar leads to catastrophic edge loading. According to ISO 281 life calculation principles, even minor misalignment in a rigid cylindrical roller bearing drastically reduces the fatigue life, resulting in sudden cage disintegration and roll damage. This unplanned downtime costs far more than the bearing itself, often requiring extensive housing re-machining and strand re-threading [NEED_CITE: impact of misalignment on bearing rating life per ISO 281].
Why Our Technical Review Prevents Caster Seizures
We do not just ship the base number; we verify the spherical seating dimensions and internal clearance against your specific caster housing drawings. Our cross-reference process explicitly checks for the convex outer ring profile and high-temperature cage materials, ensuring the replacement survives the thermal gradient. Because we hold authorized distribution across all major international brands, we can source the exact metallurgical variant you need, complete with batch traceability, eliminating the risk of soft inner rings that plague the secondary market.
Documentation & Authenticity
- Certificate of Conformity confirming the exact spherical seating tolerances for your caster housing.
- Manufacturer batch and lot traceability linking the 160 mm bore unit to the original heat treatment records.
- QR verification via official brand apps to rule out cloned codes on metallurgical bearings.
- Material test report validating the high-temperature stability of the cage and ring steel.
- Dimensional and running accuracy inspection report verifying the convex outer ring profile before dispatch.
Storage, Handling & Mounting
- Store the spherical-seat unit in its original vapor-phase inhibitor packaging until mounting to prevent corrosion on the convex outer surface.
- Use induction heating for the inner ring installation, strictly monitoring the temperature to preserve the specialized metallurgical heat treatment.
- Apply clean, heat-resistant gloves when handling to prevent acidic sweat from etching the precision-ground spherical raceway.
- Verify the housing concavity matches the bearing’s outer profile using a gauge before pressing the unit into the caster chock.
- Ensure the selected high-temperature grease is compatible with the specific shield configuration to prevent scale dust ingress.
Engineering Your Next Caster Maintenance Cycle
To ensure the replacement integrates flawlessly into your continuous caster, share the radial loads, operating temperatures, and specific housing concavity dimensions. Our engineering team will review the internal clearance requirements and cross-reference the exact spherical geometry against OEM equipment numbers. This technical validation guarantees the unit will accommodate thermal expansion without binding.
Frequently Asked Questions
Q: How do we verify the authenticity of the 160RUB32 using official channels?
A: Every unit we supply includes a unique batch code and QR label. You can scan this directly through the manufacturer’s official mobile application to verify the origin, production date, and metallurgical specifications, effectively eliminating the risk of installing counterfeit bearings with soft inner rings that fail under continuous casting loads.
Q: Why is internal clearance critical when cross-referencing this spherical-seat design?
A: In continuous casters, the inner ring runs significantly hotter than the water-cooled housing. If the cross-reference ignores the required enlarged clearance class, thermal expansion will eliminate the internal gap, causing the rollers to skid and the cage to fracture. We always verify the clearance suffix to ensure it accommodates your specific thermal gradient.
Q: What causes spherical-seat bearings to fail prematurely in steel mills?
A: Premature failures usually stem from abrasive scale dust bypassing damaged seals or improper housing machining that restricts the self-aligning capability. When the convex outer ring cannot pivot freely within the chock, the bearing acts as a rigid unit, leading to severe edge loading and early fatigue spalling on the roller ends.
Q: How do we select the correct cage material for high-temperature caster applications?
A: For the intense radiant heat near the caster mold, a machined brass cage is generally required. Polyamide cages will degrade rapidly at these elevated temperatures. We review your specific operating temperature and vibration profile to recommend the optimal cage material, ensuring structural integrity during heavy strand withdrawal operations.